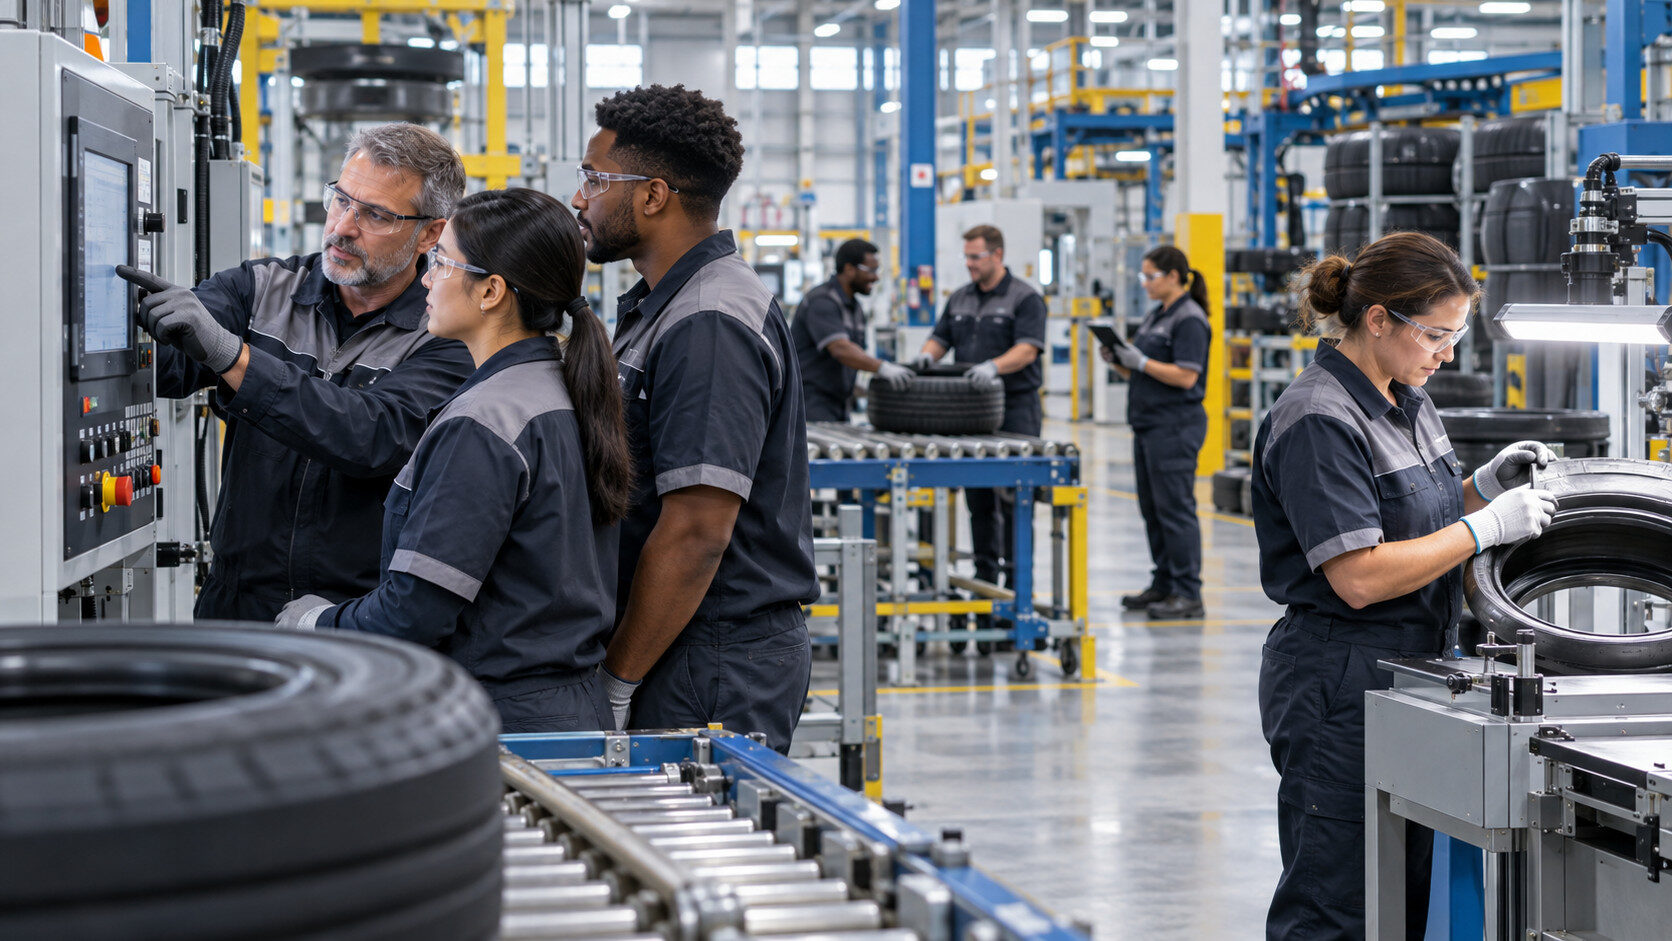
Cross-training in tire manufacturing tends to get filed under employee development, somewhere between the safety refresher and the annual review. It belongs in a different category entirely. In a tire plant, cross-training is risk management, and the plants that treat it that way absorb absences, retirements, and demand swings that put their competitors into overtime and scrap.
The test is simple. Pick your most critical station. Ask how many people on each shift can run it to rate, unsupervised, with acceptable quality. If the answer is one, you do not have a staffing plan. You have a single point of failure with a vacation schedule.
Most plants know this intuitively and still put off doing anything about it, because cross-training costs output today to protect output later, and today always feels more urgent. The result is a plant that runs well right up until the one person who understands the calender is out for six weeks.
Here is how to think about cross-training in a tire plant specifically, what the research actually supports, and where these programs usually fall apart.
The Single-Cover Problem Is Worse in a Tire Plant
Most cross-training advice is written for discrete assembly operations where stations are relatively interchangeable. Tire manufacturing is not that, and the difference matters.
A tire plant is a sequential, tightly coupled process. Mixing feeds extrusion and calendering. Those feed component prep and bead building. Those feed tire building. Building feeds curing. Curing feeds final finish and inspection. Each stage depends on upstream output and constrains downstream capacity.
That coupling changes the consequence of a gap. When an operator is missing in a discrete assembly plant, that station slows down. When your calender operator is out, you are not slowing one station, you are starving every stage behind it. When curing goes short-handed, you back up green tire inventory that has a limited shelf life before it has to be scrapped.
The stages also differ enormously in how hard they are to learn, which is the part generic cross-training programs get wrong. Tire building is a genuinely skilled job where a new operator can take months to reach rate with consistent quality. Press operation in curing is learnable faster. Mixing involves fewer people making higher-consequence decisions about compound. Final finish and inspection depend on trained judgment that is difficult to transfer and difficult to test.
A uniform policy across those stages wastes money in some places and leaves you exposed in others.
What the Research Actually Supports
The commercial case for cross-training gets quoted enthusiastically. Staffing and consulting firms report cross-trained operations seeing up to 20% higher productivity, 10 to 20% better workforce utilization, up to 30% faster recovery from disruptions such as absences or demand spikes, and turnover reductions as large as 25%. Treat those as directional vendor estimates rather than hard numbers, but the direction is consistent and matches what plant managers report.
The more useful finding comes from academic work, and it complicates the usual advice. Research published in the International Journal of Operations & Production Management used discrete event simulation to test multiple levels of cross-training against absenteeism, turnover, and process change. The finding: productivity gains from a moderate level of cross-training, on the order of two tasks per operator, outweigh the production losses that training creates. Pushing cross-training deeper than that can make system performance worse.
That is worth sitting with, because it contradicts how most programs are pitched. The goal is not an operator who can run every station in the plant. That person spends so much time training and rotating that they never reach top proficiency anywhere, and the plant pays for the training without capturing the output.
The goal is coverage depth on the stations that matter. Two people deep on every critical station, three on your constraint, and no further. That is a target a plant can actually hit in a year.
Start With a Skills Matrix, Not a Training Plan
The first move is not scheduling training. It is finding out where you are exposed, and the tool for that is a skills matrix.
Build a grid of operators against stations, and rate each operator per station on a simple scale: cannot perform, can perform with supervision, can perform independently, can perform and train others. Four levels is enough. Five if you want to separate “meets rate” from “meets rate with consistent quality.”
Then read the grid by column rather than by row. Row-wise, you see individual development, which is what HR usually looks at. Column-wise, you see coverage count per station, which is what tells you whether the plant can survive next month. Any station with one independent operator per shift is an urgent problem. Any critical station with two is acceptable. Your constraint station should have three.
For a tire plant, run this exercise with particular attention to a few predictable exposures. Mixing and compound handling, where small crews carry high consequence. The calender and extrusion lines, which are frequently one-deep. Curing press setup and bladder changes, as distinct from routine press operation. Final inspection judgment, which is often concentrated in a handful of long-tenured people. And maintenance, where the classic gap is that the mechanical techs cannot troubleshoot controls and the one electrical tech works days only.
Most plants that do this for the first time are surprised by how concentrated the risk is. It is usually four to eight positions, not forty.
Not Every Station Deserves the Same Depth
Once you can see coverage, you can spend training money where it returns something. A rough framework for a tire plant:
Deep coverage, three or more per shift. Your throughput constraint, usually curing. Any station where an unplanned gap immediately stops the line. Stations with high absence rates for whatever reason.
Standard coverage, two per shift. Most component prep, building positions within a given machine type, press operation, routine finishing.
Specialist coverage, two per plant with documented procedures. Mixing and compound, calender setup, complex press maintenance. These are roles where the learning curve is long and the pool is small. You are not trying to make them common, you are trying to make sure they are never singular. A documented procedure plus one backup beats an undocumented expert.
Judgment roles, handled differently. Final inspection and quality call-making are less about task steps and more about pattern recognition built over years. Cross-training here means structured exposure over long periods, paired review of borderline calls, and written defect standards with photographs. Two weeks of shadowing accomplishes nothing.
The point of segmenting is that it makes the program affordable. A plant trying to cross-train everyone on everything gives up and does nothing. A plant that identifies six single-cover stations and gets each one to two-deep in nine months has materially reduced its risk.
How to Cross-Train Without Losing This Quarter’s Output
The honest objection to cross-training is that it costs production, and it does. The plants that succeed manage that cost rather than pretending it away.
Train in planned windows, not peak weeks. Scheduled maintenance days, changeover periods, and seasonal slow stretches are when rotation is cheapest. Plants that decide to start cross-training in the middle of a hard quarter will stop by week three.
Rotate for weeks, not days. A one-day shadow teaches someone where the buttons are. Reaching independent competence on most tire plant stations takes a rotation measured in weeks, with the trainee working the station and the experienced operator available rather than the other way around.
Set explicit rate expectations during training. If a trainee is expected to hit standard rate from day one, they will not learn, and the trainer will take the machine back. Publish the ramp: this station runs at 70% for the first two weeks while we build the second operator, and the shift is not penalized for it.
Protect the trainer. The experienced operator teaching someone is doing two jobs. If their metrics suffer for it, they will stop teaching well, and you will not notice until the second operator turns out not to be competent. Adjust their targets for the training period or pay a trainer premium.
Verify, don’t assume. A skills matrix filled in by supervisors from memory is optimistic. Sign-off should require the operator to run the station independently for a defined period with quality within spec. Otherwise you will have a grid full of twos that is actually a grid full of ones.
Cross-Training Is a Retention Tool, Whether You Intend It or Not
The retention effect is the part plants underestimate, and in the current market it may be the larger benefit.
Tire plants and service operations across the industry are competing for a shrinking pool of experienced people. Within that market, one of the most common reasons good operators leave is not pay. It is the sense that the job is the same on year six as it was on year two, with no visible way forward.
Cross-training changes that without requiring a promotion to exist. An operator who has learned three stations has a broader job, a more credible case for a lead role, and concrete evidence the plant invested in them. Industry estimates put the turnover reduction from cross-training programs as high as 25%, and while that figure is generous, the mechanism behind it is real.
The way to capture that effect deliberately is to pay for skill acquisition. A pay progression tied to verified station qualifications, four or five steps with a real increment at each, converts cross-training from something the plant asks of people into something people pursue. It also solves the fairness problem that sinks most programs, which is that the willing operators end up carrying more responsibility for the same money as the ones who declined.
Cross-training also quietly protects institutional knowledge. Every rotation moves some of what a veteran knows into someone younger, which matters in a workforce where a substantial share of the most experienced people are within a decade of retiring. It doubles as the earliest stage of a leadership pipeline, since the operators who learn multiple stations are the ones who later become credible candidates for lead, supervisor, and eventually the roles described in our tire plant manager career guide.
Five Ways These Programs Fail
It is presented as extra work with no upside. If cross-training arrives as a mandate with no pay step and no path attached, operators correctly read it as being asked to do more for the same money, and cooperation will be minimal.
People get trained and never rotated. Skills decay. An operator qualified on the calender two years ago who has not touched it since is not coverage, though the matrix still says they are. Qualifications need periodic refresh rotations, and the matrix needs an expiry.
The matrix becomes a wall decoration. A grid built once during a lean initiative and never updated is worse than no grid, because it creates false confidence. Somebody has to own it, and it has to be reviewed monthly against actual absence and turnover.
Supervisors hoard their best people. This is the most common failure and the least discussed. A shift supervisor measured only on this shift’s output has every incentive to refuse to release their strongest operator for rotation, and to send their weakest instead. The program then trains the wrong people and produces coverage that does not hold up. The fix is structural: measure supervisors on their crew’s coverage depth alongside output, so building the bench is part of the job rather than a tax on it.
Nobody defines what qualified means. Without a written standard for each station and an objective sign-off, qualification becomes a supervisor’s opinion, and the coverage numbers stop meaning anything.
A 90-Day Starting Point
For a plant starting from nothing, the first quarter is straightforward.
In the first month, build the skills matrix for one department, not the whole plant, and read it by column to identify single-cover stations. In the second month, pick the three highest-risk stations, write or update the standard work for each, and select a second operator for each based on aptitude and interest rather than availability. In the third month, run the rotations during planned downtime with published rate expectations and protected trainers, and verify qualification with an independent run.
That gets one department from three single points of failure to zero in a quarter, with a template that transfers to the rest of the plant. It is a smaller ambition than a plant-wide program, which is exactly why it gets finished.
Frequently Asked Questions
What is cross-training in manufacturing?
Cross-training is the practice of qualifying operators to perform more than one job or station, so that the operation can cover absences, turnover, and demand changes without stopping. In a tire plant it typically means qualifying operators across stations within a department, such as multiple building machine types or press operation plus setup, and maintaining a skills matrix that tracks who is qualified on what.
How many employees should be cross-trained on each station?
Research using discrete event simulation found that a moderate level of cross-training, roughly two tasks per operator, produces productivity gains that outweigh the cost of training, while deeper cross-training can degrade system performance. In practice, aim for two independently qualified operators per shift on critical stations and three on your throughput constraint. Trying to qualify everyone on everything usually costs more in lost proficiency than it returns in flexibility.
Does cross-training reduce turnover?
The evidence suggests it helps, though the commonly cited figures come from industry rather than academic sources. Estimates of turnover reduction from cross-training programs run as high as 25%. The mechanism is credible: operators who learn additional stations have a broader job, a stronger case for advancement, and visible evidence of investment. The effect is much stronger when new qualifications come with a pay increase.
How do you start a cross-training program in a plant?
Start with a skills matrix for a single department rather than the whole plant. Rate each operator on each station, then count qualified operators per station to find single-cover positions. Fix the three highest-risk stations first: document the standard work, select a second operator, rotate them through during planned downtime with realistic rate expectations, and verify qualification with an independent run. Then repeat the pattern in the next department.
The Bottom Line
Cross-training in tire manufacturing is not a development program. It is the difference between a plant where one person’s retirement is an inconvenience and a plant where it is a crisis.
The work is unglamorous and the payoff is mostly invisible, because it shows up as problems that did not happen. But the arithmetic is favorable, the research supports a moderate and affordable version rather than an exhaustive one, and the retention benefit arrives whether you were aiming for it or not.
The plants that handle a retirement wave, a demand spike, or a flu season without scrambling are not luckier than their competitors. They spent some output last year building a bench, and they can see on a grid exactly how deep it is.
For tire and rubber manufacturers building plant capability and depth: connect with the Tire Talent team to discuss hiring for plant leadership, maintenance, and technical roles, including the specialist positions that are hardest to cover internally.
For tire industry professionals looking for an employer that invests in skills: browse current opportunities at Tire Talent or reach out confidentially to explore what your experience is worth right now.